Home / Services / Stainless Steel TIG Welding
304 and 316L stainless
We TIG weld 304 and 316L stainless from thin sheet to heavy plate, with argon back purge on the root side and heat input kept low enough that the metal stays corrosion resistant. Food plants, pharma skids, railings and custom equipment all get the same care.
304 / 316L
Argon back purge
Heat-tint control
Sanitary finishes
Short answer
Stainless steel TIG welding joins stainless with a non-consumable tungsten electrode, DC current and argon shielding gas, adding matching filler such as ER308L or ER316L by hand. It gives the tightest control of heat and bead shape of any arc process. That control, plus an argon back purge, keeps the weld free of sugaring and heavy heat tint so it resists corrosion like the base metal.
At a glance
Common alloys
304, 304L, 316, 316L; 309L filler for stainless-to-carbon joints
Filler metals
ER308L, ER316L, ER309L, ER347 for stabilized grades
Thickness range
About 0.020 in. sheet through 1/2 in. plate (multi-pass)
Current and gas
DCEN, 100% argon shield, argon back purge
Typical codes
AWS D1.6, ASME Section IX, 3-A, ASME BPE
Most stainless work that has to look good, stay clean or hold up to washdown chemicals gets TIG welded. MIG is faster on thick structural stainless, but it leaves more spatter and a wider heat-affected zone. On 16 gauge sheet or a sanitary fitting, TIG is the only process that lets a welder put down a small, flat bead and stop exactly where the joint ends.
The heat is the whole story with stainless. It holds heat about three times longer than carbon steel and expands roughly 50% more, so a welder who runs it hot gets warped panels, dark oxide on the back side and chromium carbides at the grain boundaries. We use L-grade filler, short welds and cool interpass temperatures, usually under 350°F, to keep the metal doing its job. For a side-by-side of the two processes, see our post on TIG vs MIG welding.
304 and 304L cover most equipment, hoods, tables and handrail. 316L carries molybdenum for better pitting resistance, so it shows up wherever chlorides do: brine, bleach-based sanitizers, coastal air along the Gulf. We match filler to the base metal and don't drop down a grade to save a few dollars a pound.
304 / 304L base metal: ER308L filler
316 / 316L base metal: ER316L filler
Stainless to carbon steel: ER309L, which tolerates the dilution
321 or 347 stabilized grades: ER347
Duplex 2205 on request, with the procedure your spec calls for
Prep starts with keeping carbon steel away from the part. Stainless gets its own wire brushes, grinding discs and clamps, because iron dust embedded in the surface rusts within days and looks like the weld failed. Joints are deburred and wiped with acetone before fit-up.
Fit-up is tight. On thin tube and sheet we want almost no gap, so the edges fuse without much filler. We tack on short centers and check alignment before running any real weld. A 2% lanthanated tungsten ground to a sharp point, a #8 or larger gas lens cup and a slow post-flow keep the shielding steady.
Distortion gets handled before the first tack, not after. On long seams we stitch from the middle out and alternate sides. Thin panels get clamped to copper or aluminum backing bars that pull heat out of the joint. Heavier plate gets a beveled groove, a TIG root and fill passes, with the interpass temperature checked by a temp stick between passes. Sheet from about 24 gauge up through 1/4 in. is everyday work; above that it is still doable, it just takes more passes and more time.
Then the back side. Anything with an open root gets an argon purge through dams, tape or a purge plug, and we wait until the oxygen meter reads low enough before striking an arc. A good stainless bead comes out silver to light straw on the face and nearly as bright on the root. If you want the full purge routine, it is written up in our guide to back purging stainless steel.
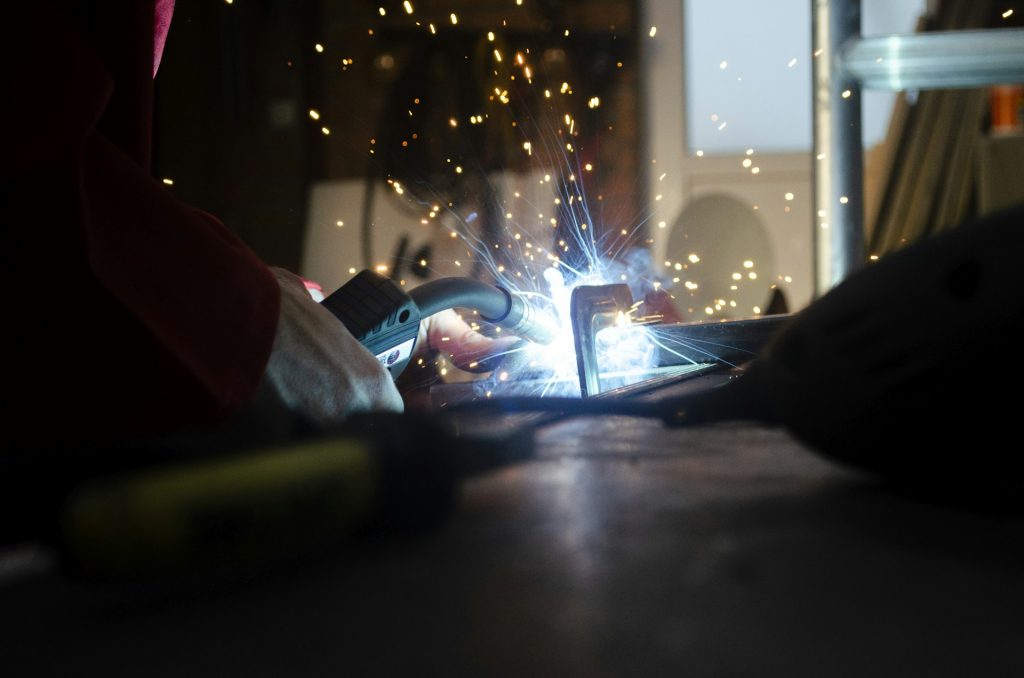
TIG torch working a stainless part on a welding table
Some tint is normal. Light straw on the face is a thin oxide that pickling removes. Blue, purple or gray means the chromium has been pulled out of the surface layer, and that spot will rust first in a wet plant. Sugaring on the root, the crusty black growth you get with no purge, is a reject on any sanitary or pressure job.
After welding we remove tint by grinding and blending, pickling paste or electrochemical cleaning, depending on the finish. Food contact surfaces can be polished to a target such as 32 Ra and then passivated to ASTM A967 with citric or nitric acid so the chromium oxide layer rebuilds evenly. Architectural parts usually get a #4 brushed blend so the weld disappears into the grain.
Tell us what the job is built to. Structural stainless falls under AWS D1.6. Pressure parts and process piping need procedures qualified to ASME Section IX, and dairy or food equipment is judged against 3-A sanitary standards. We plan the joint design, filler and inspection around the code you name.
Every weld gets a visual check for undercut, porosity, cracks and tint. Dye penetrant is a cheap way to find surface cracks on fillet welds and repair areas. When the spec calls for X-ray or a borescope look at the root, we line that up as part of the job instead of an afterthought. For tube and pipe systems built to those standards, see pipe and tube TIG welding.
Have a drawing or a photo of the part?
Text it to us or send it through the quote form. We reply with questions or a written quote.
A lot of it ends up in food and beverage plants: hoppers, chutes, conveyor guards, drip pans, kettle brackets, tank nozzles. Pharma and lab customers send skid frames and enclosures. Restaurants need hood and table repairs. Architects and contractors bring us handrail, guardrail, column wraps and stair stringers that have to look like one piece.
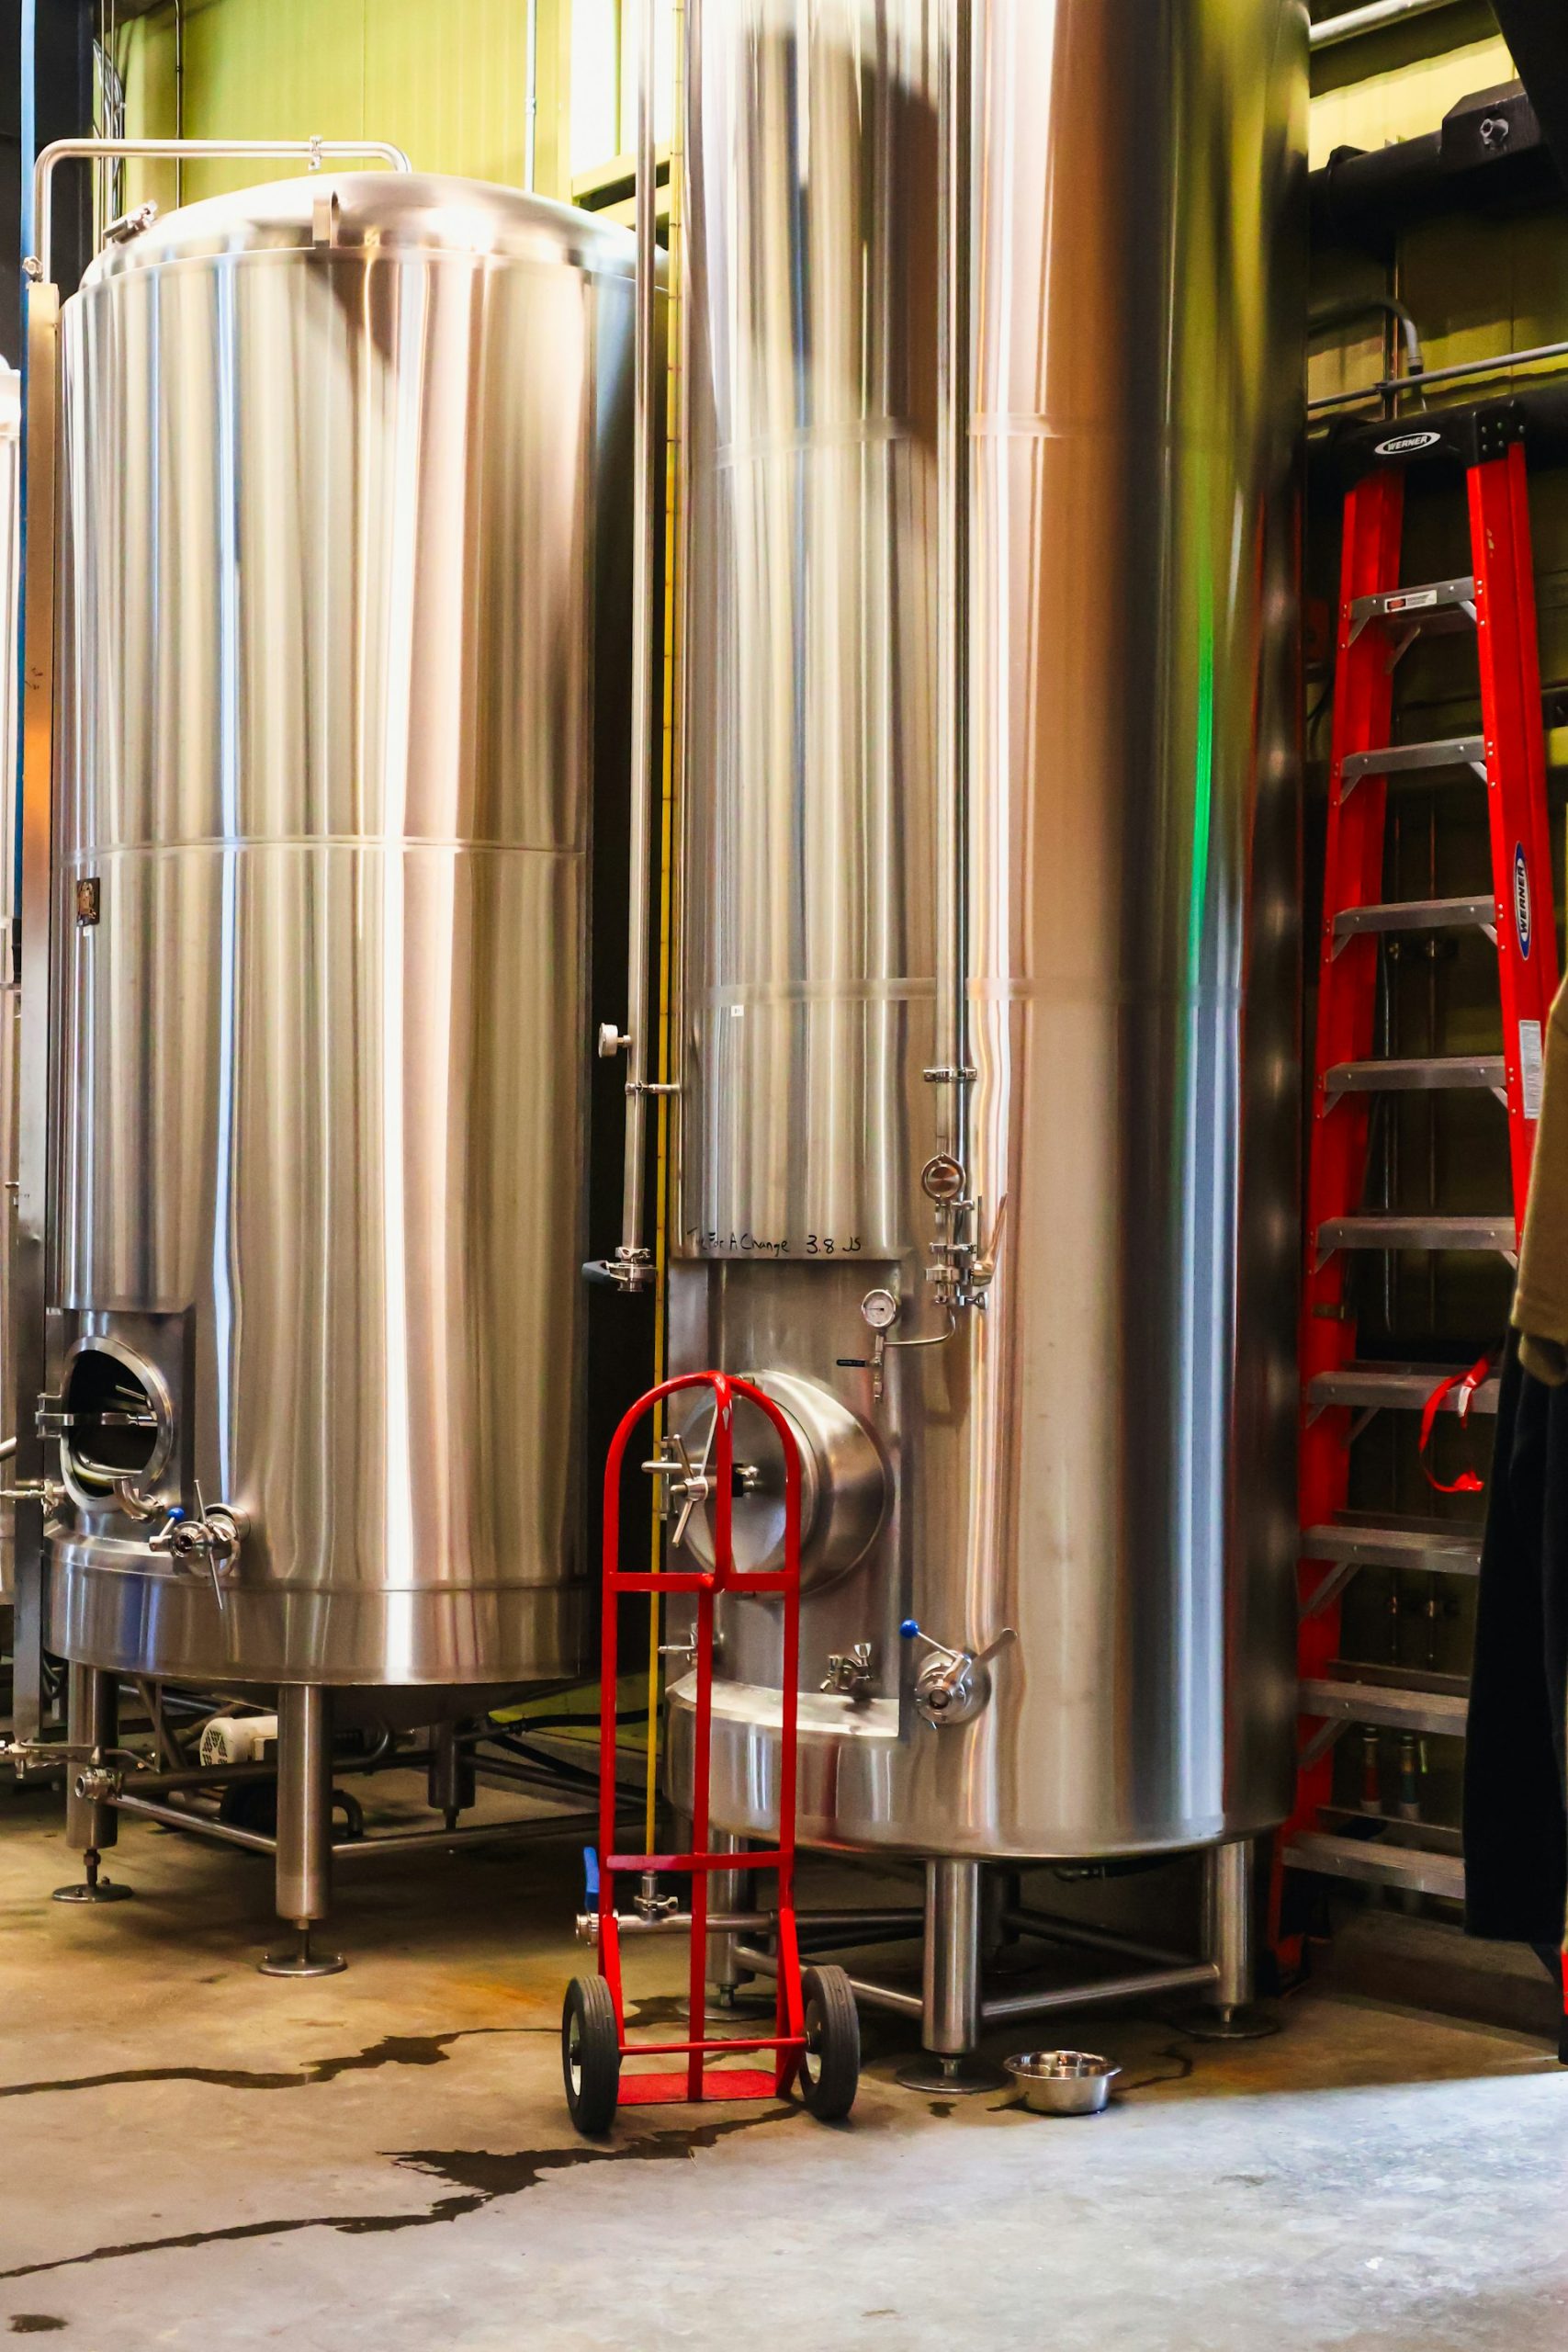
Boat owners along the coast bring 316 bow rails, T-top fittings and davits, since 304 tends to tea-stain in salt spray. Brewers send fermenter legs, ports and racking arms. Most of this is done in the shop, where purge, fixturing and finishing are easier to control. Installed tanks, rail that is already anchored and plant equipment that can't come out are a different job, and those we handle on site.
A drawing helps, but a phone photo with a tape measure in the frame gets us most of the way. Send it through the contact page or call (346) 561-0862.
Grade, if you know it (304, 316L, or check the mill cert)
Thickness or gauge, and tube OD and wall
Is it food contact, pressure, structural or cosmetic
Finish you need: as-welded, #4 brushed, polished, passivated
Code or customer spec, if any
Quantity and the date you need it
Can you TIG weld 304 to 316 stainless?
Yes. 304 and 316 weld together without trouble. Most welders use ER316L filler so the joint is at least as corrosion resistant as the 304 side, though ER308L is acceptable in mild service. Purge the back side as you would for either grade alone. In chloride or sanitizer exposure, go with 316L filler and treat the whole assembly as 316L for cleaning and passivation.
Why does my stainless weld look black or crusty on the back?
That is sugaring. Without argon on the root side, oxygen attacks the hot metal and leaves a rough, oxidized crust. It traps bacteria, starts corrosion and is rejected under any sanitary or pressure standard. The fix is to back purge with argon before and during welding. Sugared welds usually have to be cut out and redone, because grinding rarely removes all of it.
Do stainless welds need to be passivated?
Not every weld, but anything in food contact, chemical service, or wet and salty air benefits from it. Welding and grinding leave free iron and a damaged oxide layer. Pickling removes heat tint, and passivation with citric or nitric acid per ASTM A967 restores a uniform chromium oxide film. Indoor decorative parts often only need tint removal and a brushed finish.
What is the difference between 304 and 316L for welding?
Both weld much the same way with TIG. 316L contains 2 to 3% molybdenum, which resists pitting from chlorides, and the L means low carbon, under 0.03%, which limits carbide formation near the weld. 304 is cheaper and fine indoors and in many food plants. For coastal Texas, brine, bleach sanitizers or pharma water, 316L is the safer choice.
How thin can you TIG weld stainless steel?
With a pulsed inverter, a sharp tungsten and good fit-up, TIG handles stainless down to roughly 0.020 in., about 24 gauge. Thin sheet and tube need tight joints with no gap, copper or aluminum chill bars to pull heat away, and short welds stitched around the part. Below that thickness, joints are often edge-flanged so they can be fused without filler.
Will a welded stainless railing rust?
It shouldn't, if it is done right. Rust on stainless rail usually comes from carbon steel contamination, heat tint left on the weld, or 304 used near salt water. We use stainless-only tools, remove tint after welding and blend the joint. On the coast or near pools, 316 tube with a polished finish holds up far better than 304 with a brushed one.
Pipe & tube
TIG root passes on process pipe, sanitary tube and chromoly, with purge, fit-up and inspection planned around B31.3, B31.1, 3-A or BPE.
See the service →
Custom fabrication
One-offs and short runs cut, formed, fitted and TIG welded: brackets, frames, enclosures, tanks, rails and prototypes.
See the service →
Weld repair
Cracked aluminum and stainless parts, cast aluminum, cast iron and failed welds, repaired after we find out why they broke.
See the service →
Get a quote
Send drawings, photos or a short description. We reply with questions or a written quote.
Request a quote